 New
Custom Machining
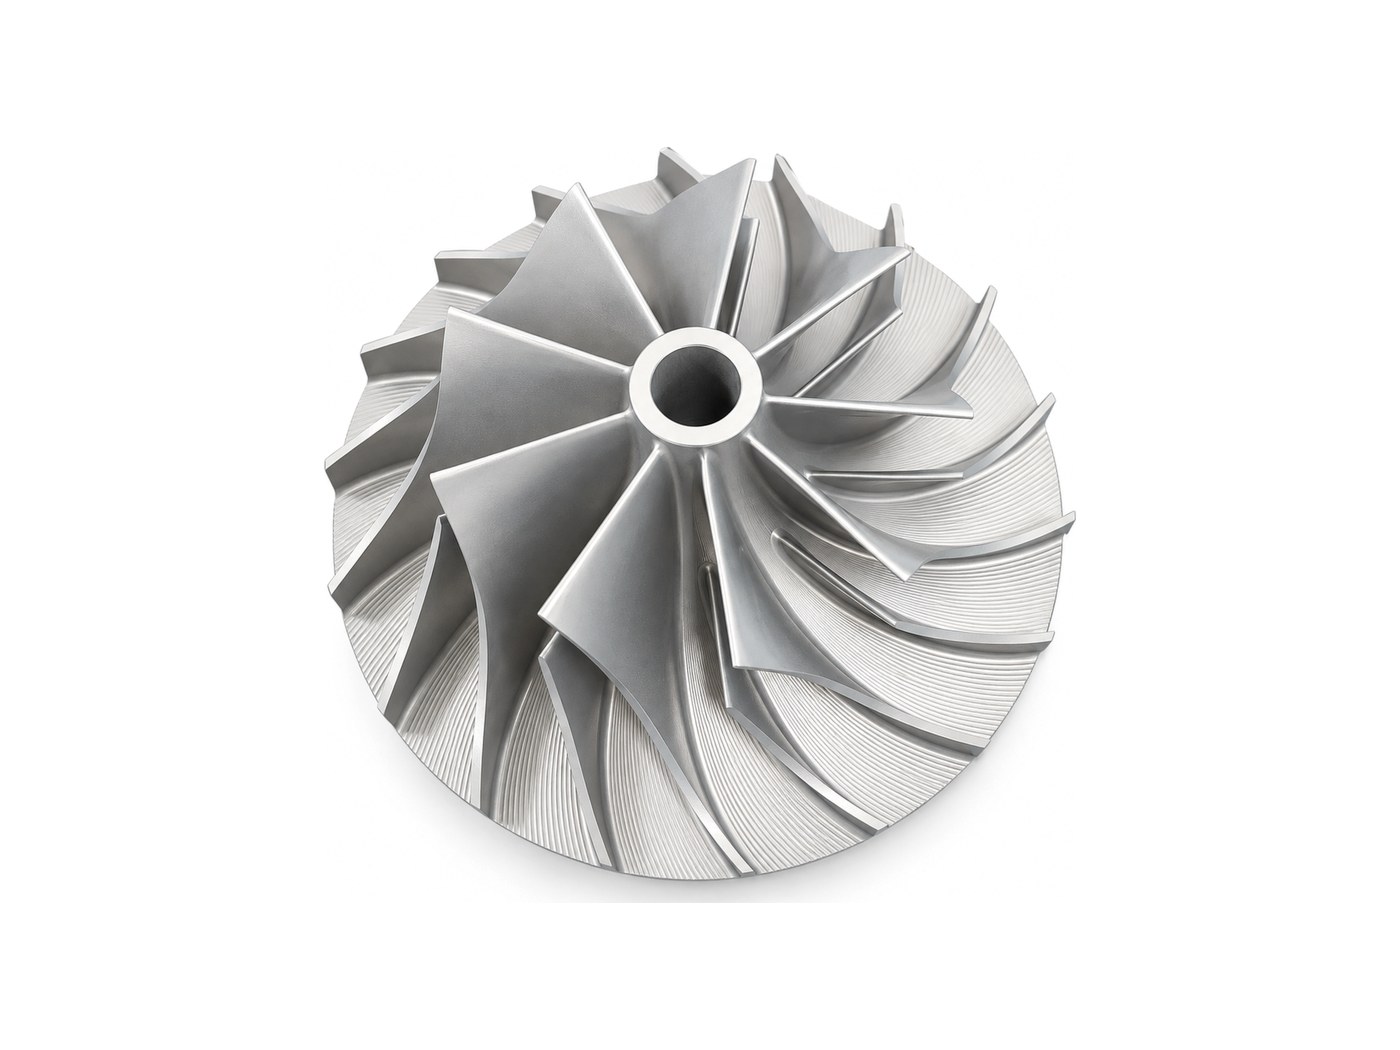
Custom CNC Machining Service
Send a drawing or a sample — get a manufacturability review and a firm quote.
View MACHININGDongguan Hairuixing Technology Co., Ltd.
Finish is not decoration — it is corrosion protection, wear resistance and a controlled surface for sealing or bonding. We manage anodising, passivation, electropolishing, plating and bead blasting through audited finishing partners, with masking plans and thickness checks so a housing comes back the colour and thickness the drawing asked for.
| Anodising | Type II (decorative) and Type III (hardcoat) |
|---|---|
| Hardcoat thickness | 25–50 µm, up to 75 µm on request |
| Colours | Black, natural, red, blue, gold, grey, custom |
| Passivation | ASTM A967 / AMS 2700 for stainless steel |
| Electropolishing | Medical and food-grade finish, Ra improvement |
| Other finishes | Bead blasting, brushing, nickel / zinc plating, laser marking |
| Masking | Threads, bores and sealing faces masked to drawing |
| Lead time | adds 3–7 working days |
Anodising adds roughly half the coating thickness to a surface and half into it, which changes thread fits and bore sizes. We agree a masking and dimension plan before treatment, so threads gauge and bores stay in tolerance afterwards.
Anodised colour drifts with alloy, bath temperature and time. We process a batch together, keep reference samples and check against them — so the enclosure you order next quarter matches the one on the shelf.
Type III hardcoat gives 25–50 µm of wear-resistant oxide, useful on sliding surfaces, fixtures and parts that see repeated assembly. It also dulls the colour range, so we recommend it for function rather than appearance.
Passivation to ASTM A967 with test records, RoHS and REACH statements, and coating thickness reports for hardcoat are available. Ask on the enquiry: the certificate has to be ordered with the job, not added later.
Yes. The coating grows roughly half outward and half inward, so bores get smaller and shafts get larger. We agree which surfaces must be masked and which must be machined to pre-treatment size before the job starts — tell us the fits that matter on the drawing.
Standard Type II is for appearance and general corrosion protection with a wide colour range. Type III hardcoat is thicker and far more wear-resistant but has a narrower, duller colour range. If the part slides, clamps or is assembled repeatedly, choose hardcoat; if it is an enclosure you want to look right, choose Type II.
To a practical degree, yes. We keep a reference sample from your first batch and check subsequent batches against it. Exact matches are limited by alloy batch and bath condition, so for critical appearance parts we advise ordering the full quantity at once.
Yes. Sealed anodising and passivated stainless are commonly specified with salt-spray exposure per ISO 9227 or ASTM B117. State the required hours on the enquiry so we select the right seal and can arrange testing with the batch.
New
Send a drawing or a sample — get a manufacturability review and a firm quote.
View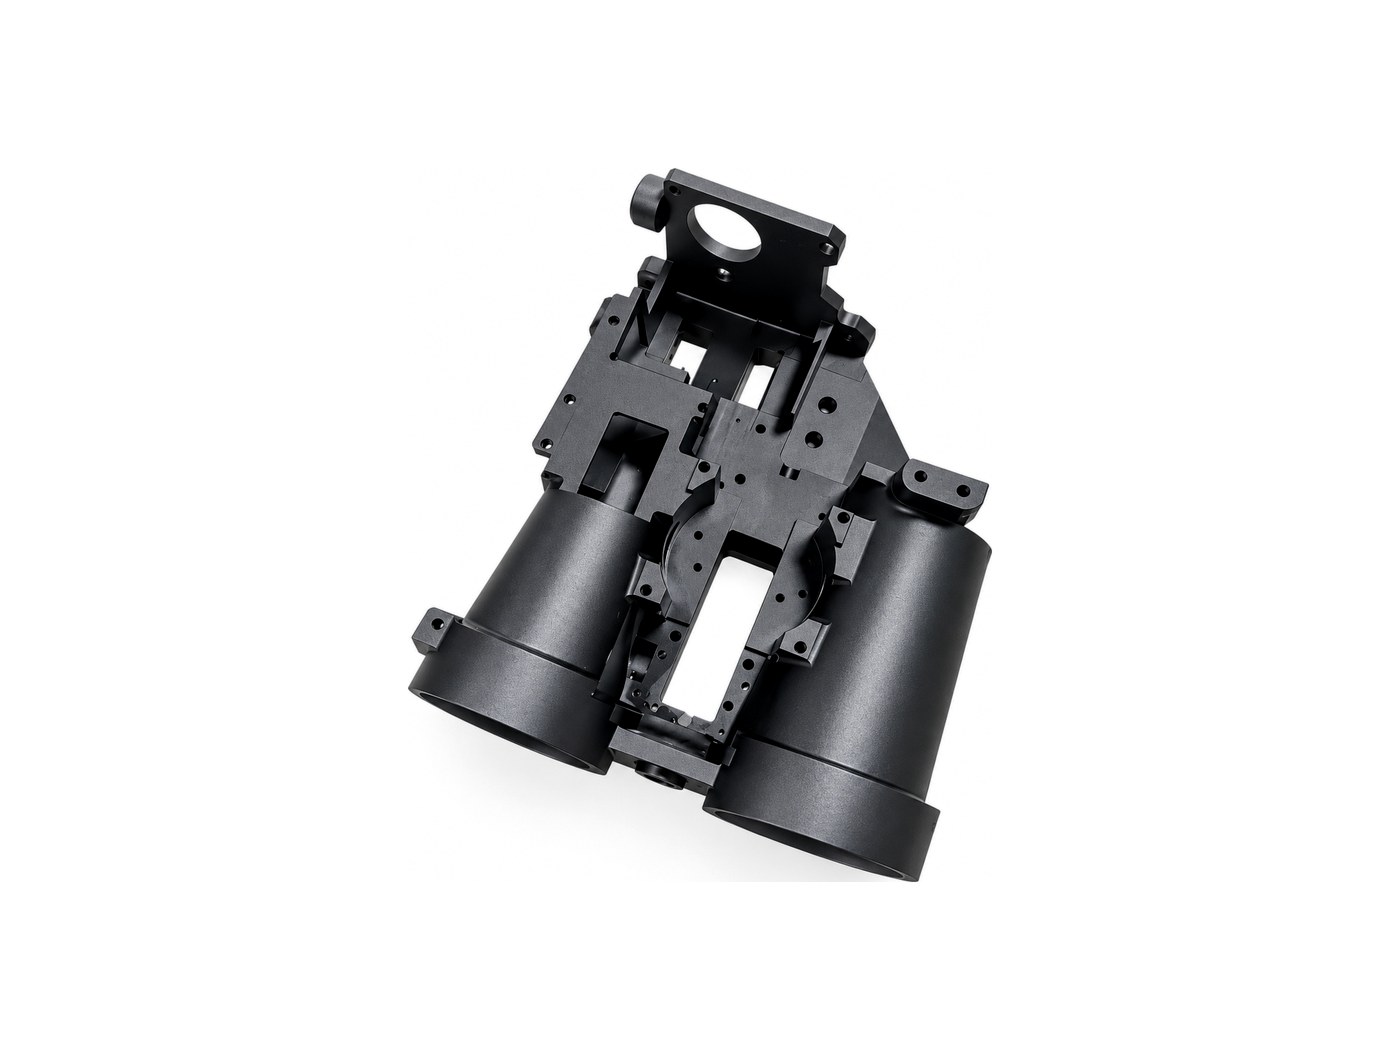
Thin-wall tubes, binocular bodies, baffle cones and eyepiece holders — machined to one datum.
View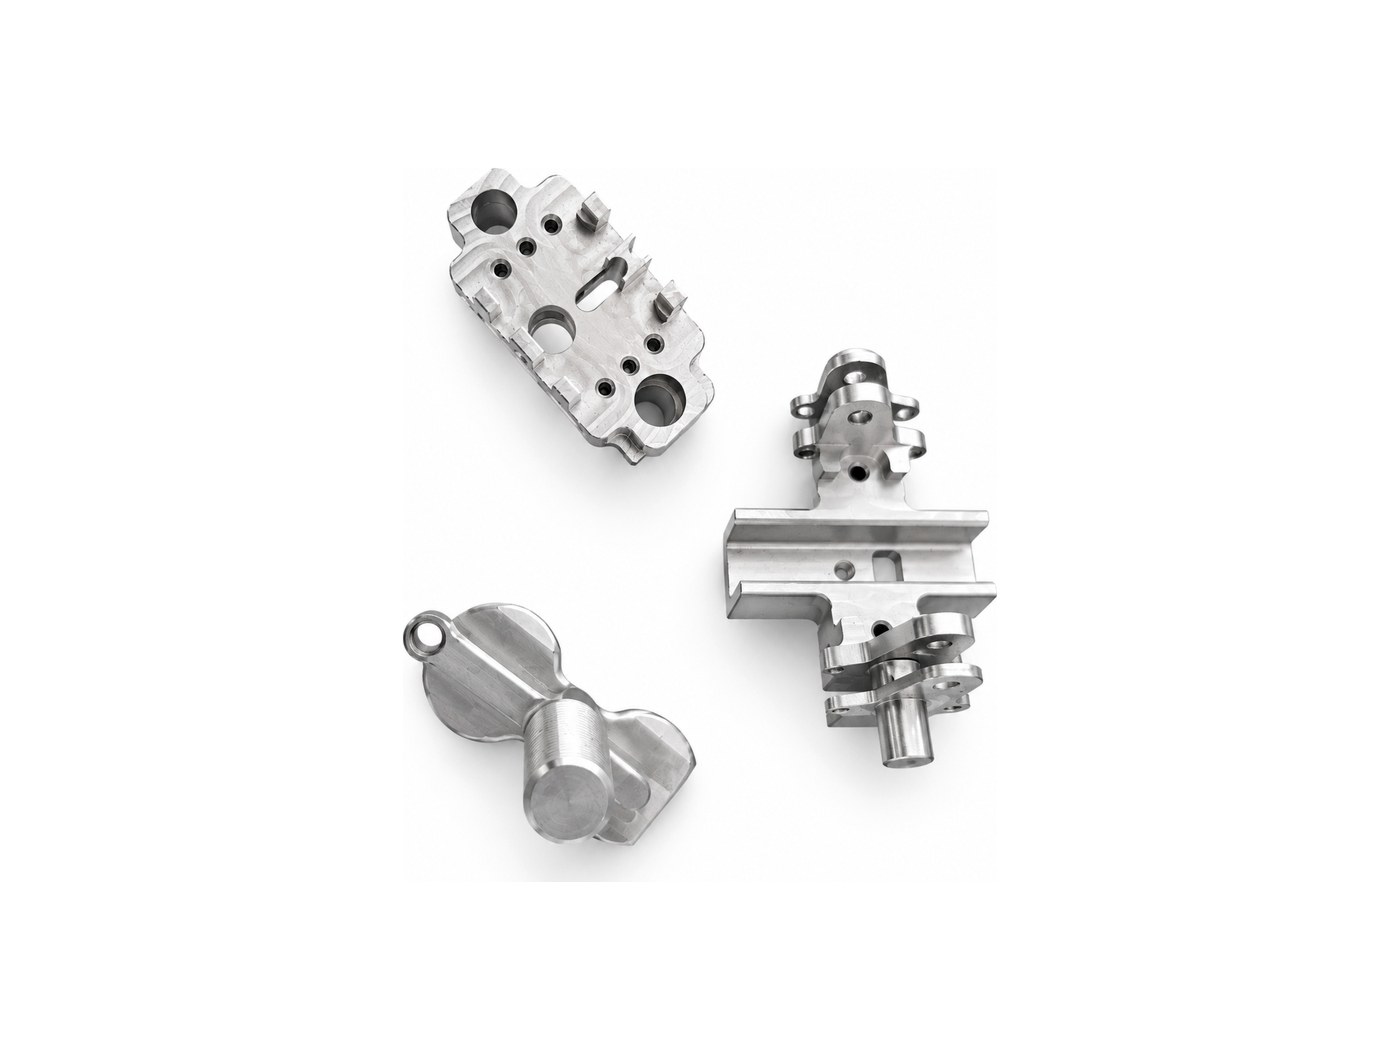
Instrument bodies, bone plates, drill guides and implant trial components.
ViewSend your drawing and receive a manufacturability review plus firm pricing within 24 hours.